logo
Supal (Changzhou) Precision Tools Co.,Ltd
회사 소개
당신의 전문적이고 신뢰할 수 있는 파트너
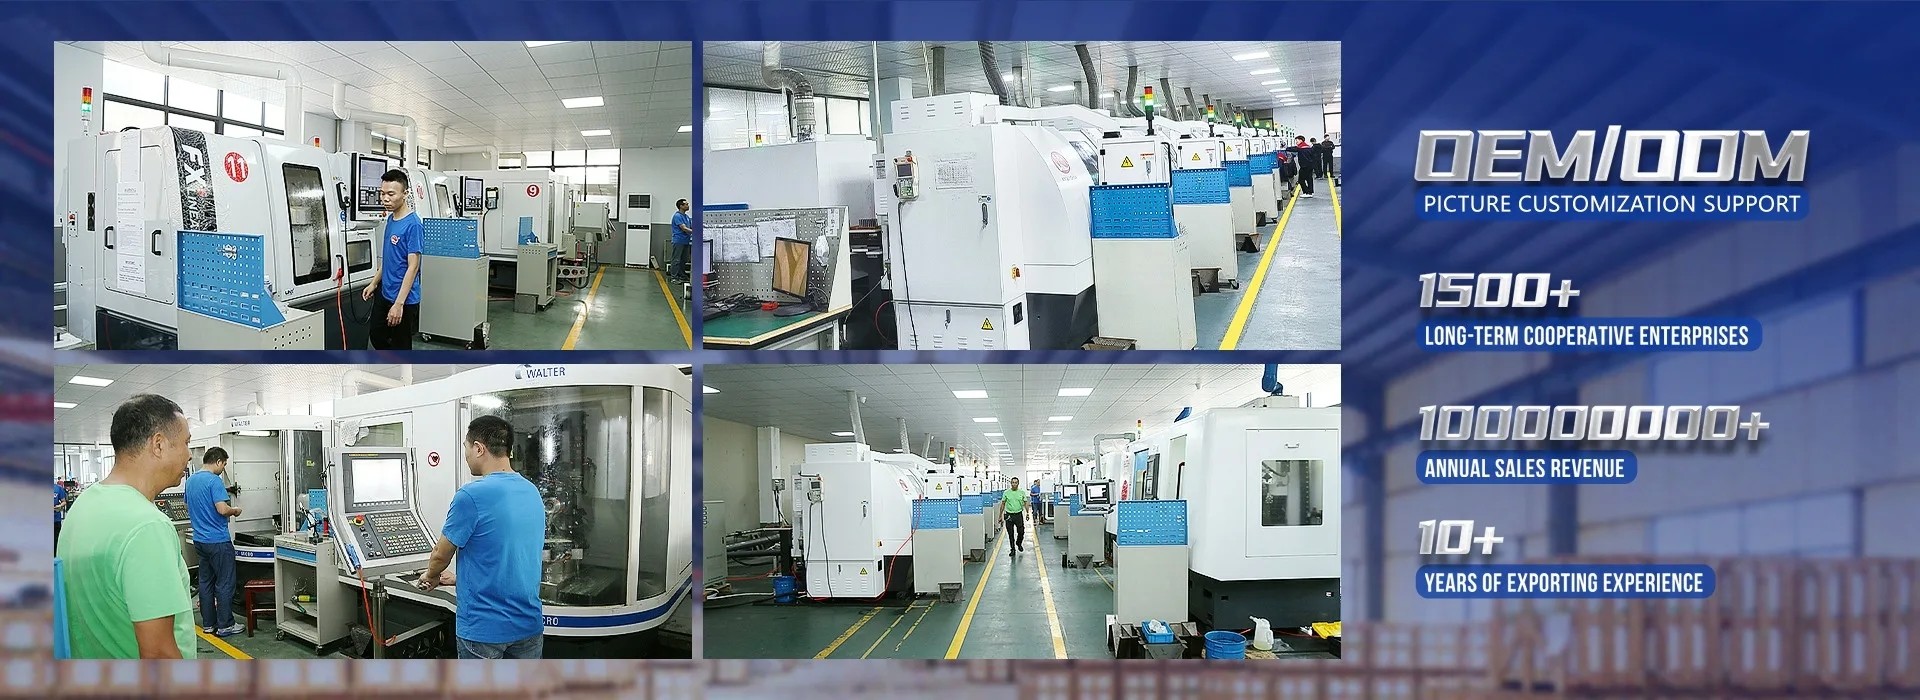
수팔 (창저우) 정밀 도구 회사많은 년 동안 고체 탄화물 도구의 설계, 생산 및 마케팅에 종사했으며, 총 투자액은 1천만 달러 이상이며 경험이 많은 직원들로 구성됩니다.전문 도구 제조업체로서, 그것은 창저우 Xiaxiashu 도구 협회의 이사회 회원 중 하나가되었습니다. 회사는 독일의 월터와 슈테를 소개했습니다.오스트레일리아의 ANCA 및 5계각 NC 절단 썰기또한, 회사는 ZOLLER의 자르는 자동 탐지기와 EUROTECH의 PG1000 초정밀 다기능 탐지기를 갖추고 있습니다.회사의 주요 제품은: 고체 탄화물 깎기, 구멍 처리 깎기; 또한,우리는 또한 설계하고 고객의 요구 사항에 따라 다양한 비 표준 절단기를 생산 할 수 있습니다우리의 제품은 국내 항공, 자동차, 기계, 곰팡이, 플라스틱, 전자, 의료 기기 및 기타 고 정밀 마무리 분야에서 광범위하게 사용되었습니다."건전성 기반, 고객 최우선"의 서비스 철학과 "품질에 생존하고 신용에 의해 발전"의 목표를 바탕으로회사는 고객들에게 ...
더 배우세요

0

확립된 년 :

0

백만+
직원

0

백만+
연간 매출 :
중국 Supal (Changzhou) Precision Tools Co.,Ltd 고품질
신뢰 표지판, 신용 점검, RoSH 및 공급자 능력 평가 회사는 엄격한 품질 관리 시스템과 전문 테스트 실험실을 갖추고 있습니다.
중국 Supal (Changzhou) Precision Tools Co.,Ltd 개발
내부 전문 설계 팀과 첨단 기계 작업실 우리는 당신이 필요로 하는 제품을 개발하기 위해 협력할 수 있습니다.
중국 Supal (Changzhou) Precision Tools Co.,Ltd 제조업
첨단 자동 기계, 엄격한 프로세스 제어 시스템. 우리는 당신의 요구 이상의 모든 전기 단말기를 제조 할 수 있습니다.
중국 Supal (Changzhou) Precision Tools Co.,Ltd 100% 서비스
대용품 및 맞춤형 소형 패키지, FOB, CIF, DDU 및 DDP. 우리는 여러분의 모든 고민에 대해 최선의 해결책을 찾을 수 있도록 도와드리겠습니다.

품질 탄화물 밀링 공구 & 사각 엔드밀 제조업체

더 당신의 요구를 만족시킨 제품으로 찾으세요.
사건 및 뉴스
최신 핫 스팟
Corner Radius vs Square End Mills for Interrupted Shoulder Milling
Corner Radius vs Square End Mills for Interrupted Shoulder Milling Interrupted shoulder milling is one of the operations where end mill geometry has a direct effect on edge stability. When the cutter repeatedly enters and exits the workpiece, passes across gaps, or encounters uneven stock, each tooth experiences a changing load instead of a smooth continuous cut. A square end mill can produce a sharp 90-degree shoulder, while a corner radius end mill can distribute load around the tool corner and reduce local stress. Choosing between them requires more than looking at the drawing requirement. For CNC machinists, process engineers, and purchasing engineers, the correct decision depends on the balance between required corner definition, interruption severity, tool rigidity, material, engagement, and finishing strategy. This guide compares square and corner-radius geometries for interrupted shoulder milling and explains how to diagnose edge chipping, chatter, poor finish, and unstable tool life. What Makes Interrupted Shoulder Milling Difficult? In a continuous side-milling cut, the cutting edge enters the workpiece and remains engaged in a relatively predictable way. In an interrupted shoulder operation, the edge may encounter a slot, a cross-hole, a casting irregularity, a forged surface, a previous pocket, or an open boundary. Each interruption changes the force and can create impact at entry or exit. The highest-risk conditions usually include: Repeated entry and exit at the same corner of the tool Full radial engagement at a 90-degree shoulder Thin walls or weak workholding that move during the cut Long tool overhang or poor holder runout Abrasive scale, cast skin, or hard inclusions Excessive feed or engagement at the interruption point A sharp square corner exposed to repeated impact A tool can therefore fail even when the average cutting load appears acceptable. The peak impact load, not only the average spindle load, may determine whether the edge survives. Square End Mills: Strengths and Limits A Square End Mill is the natural choice when the part requires a sharp internal shoulder or a flat-bottomed slot. Its geometry can produce a defined 90-degree corner without leaving a programmed radius at the bottom of the wall. When a Square End Mill Is Appropriate Square end mills are often considered when: The finished feature requires a sharp shoulder The toolpath uses stable, continuous engagement The workpiece and fixture are rigid The interruption is limited or can be approached with a controlled entry A separate finishing pass can protect the final corner quality The tool diameter and reach provide sufficient core strength A square tool can perform well in interrupted milling when the edge is properly supported and the engagement is controlled. It should not be rejected simply because the cut is interrupted; the severity and location of the interruption matter. Where Square Corners Become Vulnerable The tool corner is a stress concentration. During an interrupted cut, the corner may take a sudden impact as it enters the material. If the tool is also deflecting, the corner can receive more load than the other flutes. Typical results include corner chipping, a small radius appearing on the part after wear, chatter marks, or an abrupt change in surface finish. A sharp corner can also be sensitive to hard spots, scale, and thin-wall movement. If the failure is concentrated at the corner while the side cutting edges remain relatively intact, geometry and engagement should be reviewed before changing coating alone. Corner Radius End Mills: Strengths and Limits A Corner Radius End Mill includes a controlled radius between the end face and peripheral cutting edge. The radius removes the most fragile sharp corner and distributes cutting load over a larger region of the tool tip. When a Corner Radius Is Advantageous A corner-radius tool is often considered when: The cut includes repeated entry and exit The operation encounters an interrupted or uneven surface Edge chipping is concentrated at a square corner The part drawing permits a small internal radius The operation uses higher engagement or heavier roughing The process needs additional corner strength and more stable tool life The radius does not eliminate vibration or poor setup conditions, but it can reduce the severity of a localized corner impact. It may also improve the tool’s tolerance of intermittent engagement when compared with an otherwise similar sharp-corner tool. The Geometric Trade-Off The main limitation is straightforward: a corner radius leaves a radius on the finished shoulder. If the part requires a sharp 90-degree internal corner, the radius may need to be removed by a secondary operation or replaced by a square finishing tool. A corner radius can also change the effective engagement and contact area. It should be evaluated together with axial depth, radial engagement, tool diameter, and the required surface finish rather than selected based on radius size alone. How to Choose Between the Two Geometries Start With the Drawing Requirement First identify whether a sharp internal corner is functionally required or simply shown as a nominal feature. If a small radius is acceptable, a corner-radius tool may provide a more robust roughing or semi-finishing process. If a sharp corner is essential, use a square tool where practical or plan a roughing-and-finishing sequence that controls the load on the final square edge. Identify the Interruption Type Not all interruptions have the same effect. A predictable open boundary may be easier to manage than a hard casting skin or an irregular forged surface. Cross-holes and slots can create repeated impact at a known location, while uneven stock can make the load unpredictable. Record where the first damage occurs. If chipping starts at every entry point, the issue may be impact or lead-in strategy. If it appears only at a particular section of the workpiece, inspect material condition and support at that location. Match the Tool to the Operation For roughing and semi-finishing, the added corner support of a radius can be valuable when the operation is interrupted. For finishing, a square tool may be preferred if the corner specification requires it and the setup can maintain stable engagement. A practical process may use a corner-radius tool for stock removal, followed by a square end mill for the final shoulder. The two tools should not automatically use identical cutting conditions; the finishing tool may require a different engagement and a more controlled pass. Geometry, Edge Preparation, and Coating Edge Preparation A completely sharp edge may reduce cutting force in some materials, but it can be vulnerable to impact. A lightly reinforced edge may provide better stability in interrupted cuts, although excessive edge honing can increase rubbing and heat. The appropriate edge preparation depends on the workpiece, interruption severity, tool diameter, and operation. When comparing tools, request information about edge preparation rather than evaluating only flute count or coating name. Two tools with similar descriptions may behave differently if their edge preparation and carbide substrate differ. Helix and Flute Configuration Helix and flute count influence force direction, chip evacuation, and the number of teeth sharing the load. A higher flute count may support feed capacity in a light radial finishing pass, while a roughing or interrupted operation may need more chip space and a stronger core. The right balance depends on the material and engagement. A tool with insufficient flute space may recut chips, while a tool with a very thin core may lack impact resistance. Select from the broader Carbide Milling Tools range based on the actual operation rather than relying on the end mill shape alone. Coating Coating should follow the dominant failure mechanism. A coating may help manage heat, adhesion, or abrasive wear, but it cannot compensate for excessive tool deflection, a sharp corner overloaded by impact, or an unstable fixture. If the tool chips at entry, check geometry and rigidity before assuming that a coating change is the primary solution. Any coating recommendation should be validated with the specific material, tool geometry, coolant strategy, and cutting conditions. Treat supplier data as a starting reference and confirm the result on the actual machine. Parameter Strategy for Interrupted Shoulder Milling Cutting data should be treated as a starting reference for the exact diameter, flute count, coating, material grade, tool overhang, and machine setup. Do not transfer a value from a continuous side-milling operation directly to an interrupted shoulder cut without validation. Control the Peak Load at Entry Entry conditions can create the highest impact. Where the geometry allows, use a ramp, arc, or controlled lead-in instead of an abrupt radial plunge. This reduces the sudden change from no load to full engagement. If a direct entry is unavoidable, review feed and radial engagement at the entry point. A controlled reduction in engagement or a separate approach pass may protect the edge better than reducing the entire program feed. Avoid Excessive Full-Width Engagement Full-width shoulder milling creates significant radial load. In an interrupted condition, the load can change sharply as the tool crosses the gap. If possible, use a reduced radial engagement strategy for roughing and leave a controlled allowance for finishing. The correct engagement depends on the tool, material, machine, and feature geometry. Validate changes with spindle load, sound, chip form, and edge inspection rather than assuming that a smaller engagement is always better. Adjust Speed and Feed One Variable at a Time If the tool chips, do not immediately reduce both speed and feed. First determine whether the damage is impact-related, vibration-related, or caused by rubbing. A feed reduction that is too large can create a thin chip and increase rubbing, while a speed change may affect heat and resonance differently. Change one parameter at a time and document the effect. Include the location of the failure, chip appearance, surface finish, and tool condition in the record. Diagnosing Common Failure Symptoms Corner Chipping on a Square End Mill Check interruption severity, tool entry, runout, edge preparation, and whether the square corner is taking the full impact. If the drawing permits it, compare a corner-radius tool in the roughing or semi-finishing stage. If a square corner is mandatory, reduce entry shock and ensure the finishing pass has consistent stock. Chatter on a Corner-Radius Tool A radius does not remove the need for rigidity. Check tool overhang, holder condition, workholding, spindle speed, axial depth, and radial engagement. Chatter may also result from a radius that creates an engagement pattern unsuitable for the current toolpath. Uneven Wear Between Flutes Uneven wear commonly points to runout, unequal flute loading, poor holder seating, or a workpiece that is moving. Inspect the shank, collet, holder, and setup before changing the tool geometry. Poor Shoulder Finish After Roughing A roughing tool with a damaged corner or built-up edge should not be used for a critical finishing pass. Clean the feature, use a sound finishing tool, and verify that the remaining allowance is consistent. If the finish still varies, inspect vibration and workholding. Short Tool Life at a Hard Spot If damage occurs only at a particular location, investigate material condition, scale, interrupted geometry, or inadequate support. A different corner geometry may help, but the toolpath and entry strategy should also be reviewed. Common Mistakes to Avoid Choosing a Square Tool Only Because the Part Has a 90-Degree Corner A square finishing tool may be correct for the final feature but unnecessarily vulnerable during heavy interrupted roughing. Separate stock removal from final corner generation when the process requires both robustness and a sharp corner. Assuming a Corner Radius Always Solves Chipping The radius can improve corner strength, but it does not fix excessive overhang, runout, unstable workholding, poor parameters, or a damaged holder. Reducing Feed Aggressively After Chipping A large feed reduction can cause rubbing and heat. Determine whether the first damage occurred at entry, during an interruption, or under continuous cutting before making broad changes. Ignoring Toolholding The geometry selected on paper cannot compensate for poor holder cleanliness, excessive runout, or unnecessary projection. Check the actual holder and machine setup. Mixing Roughing and Finishing Requirements One tool rarely provides the best combination of high interruption tolerance, high stock-removal capacity, sharp 90-degree finishing, and final surface quality. Define which pass is responsible for each requirement. FAQ Is a corner radius end mill stronger than a square end mill? The radius removes the sharpest corner stress concentration and can improve resistance to local chipping in some interrupted operations. The actual result still depends on material, edge preparation, tool diameter, engagement, rigidity, and parameters. Should I use a corner radius for every interrupted shoulder cut? No. If a sharp 90-degree corner is required, a square end mill may still be necessary for finishing. A corner-radius tool can be considered for roughing or semi-finishing when the part permits a radius or a secondary finishing operation. Why does my square end mill chip only at the entry point? The entry may create an impact or engagement spike. Check lead-in strategy, radial engagement, feed at entry, runout, workpiece support, and the condition of the material surface at the entry location. Can changing the coating stop corner chipping? Only when the dominant failure involves heat, adhesion, or wear that the new coating is suited to control. Coating cannot correct an overloaded corner, poor rigidity, abrupt entry, or excessive engagement. What information should I provide when requesting an end mill recommendation? Provide the material grade, shoulder and interruption geometry, required corner condition, tool diameter and reach, machine and holder details, current parameters, coolant method, tool wear pattern, and photographs of the damaged edge or finished shoulder. Conclusion The choice between a corner-radius and square end mill for interrupted shoulder milling should begin with the part requirement, then consider interruption severity, edge strength, tool rigidity, engagement, and finishing strategy. A square end mill provides a sharp corner but concentrates stress at the tool tip. A corner-radius end mill distributes load more gradually and may reduce local chipping when a radius is acceptable. For demanding operations, a two-stage process can balance both objectives: use a robust geometry for interrupted roughing or semi-finishing, then use a square tool for the final shoulder when the drawing requires a sharp corner. Build parameters from the supplier’s starting range, change one variable at a time, and validate the complete process on the actual machine and workholding. If your shoulder milling process shows corner chipping, chatter, poor finish, or inconsistent tool life, Contact Supal with the material grade, interruption geometry, current tool, tool overhang, parameters, and photos of the failure. This information helps identify a practical geometry and process starting point for on-machine validation.

2026

10/06

How to Choose Carbide End Mills for Copper and Brass Machining
How to Choose Carbide End Mills for Copper and Brass Machining Copper, brass, bronze, and other copper alloys are often described as easy-to-cut materials because they are softer than hardened steel. That description can be misleading. Copper alloys can create very different machining problems depending on their purity, temper, alloying elements, work-hardening behavior, and chip form. A tool that produces a clean result in free-machining brass may rub, smear, or generate built-up edge in a more adhesive copper grade. For CNC machinists, process engineers, and purchasing engineers, reliable copper alloy milling starts with matching the tool to the actual failure mechanism. Edge sharpness, flute space, chip evacuation, workholding, coolant, and parameter validation usually matter more than simply choosing the hardest or most expensive coating. This guide explains how to select carbide end mills for copper and brass machining while reducing adhesion, burrs, heat, and unstable tool life. Why Copper and Brass Need Material-Specific Tool Selection Copper alloys combine several characteristics that influence milling stability: Copper conducts heat efficiently, so heat can move into the workpiece instead of remaining concentrated at the tool edge. However, local rubbing can still raise edge temperature and cause adhesion. Pure or highly ductile copper can produce continuous, gummy chips that are difficult to evacuate. Brass and bronze grades vary widely. Some produce short chips, while others create longer chips or abrasive particles. A dull edge may rub and smear the surface rather than shear it cleanly. Thin walls, small features, and poor workholding can amplify deflection and burr formation. The result is that “copper” or “brass” is not enough information for final tool selection. The exact alloy or grade, hardness or temper condition, feature geometry, and finishing requirement should be confirmed before adopting a production tool. Common Failure Symptoms in Copper Alloy Milling Built-Up Edge and Material Adhesion Built-up edge appears when copper or another ductile alloy adheres to the cutting edge. The tool may look sharp at the beginning of the cut but gradually develops a welded mass that changes the effective edge geometry. This can cause poor surface finish, burrs, dimensional variation, and sudden edge damage when the built-up material breaks away. Adhesion is often promoted by rubbing, insufficient chip evacuation, a dull edge, excessive dwell, or a surface treatment that is not suited to the material. Changing to a harder coating without correcting rubbing may not solve the problem. Smearing and Poor Surface Finish A smeared surface usually indicates that the tool is not shearing the material cleanly. Possible causes include insufficient chip thickness, a dull or heavily honed edge, poor tool runout, unstable workholding, or a speed/feed combination that leaves the tool rubbing instead of cutting. Burrs at Entry and Exit Copper and brass can produce burrs when the cutting edge pushes material away at the exit. Burr formation is influenced by tool sharpness, radial engagement, feed direction, workpiece support, and the condition of the edge. A finishing pass may reduce burrs, but the root cause should still be addressed in the toolpath and tool selection. Chipped Edge or Unexpected Tool Failure Carbide edge chipping in copper alloy milling is not always caused by a material that is too hard. Interrupted cuts, loose workholding, excessive runout, thin-wall deflection, collisions, and trapped chips can generate impact loads that damage the edge. If chipping is concentrated on one flute, inspect runout and setup balance before changing the carbide grade. Chip Packing and Recutting Long copper chips can remain in a pocket, slot, or narrow cavity. Once recut, they create additional heat and load, increasing the chance of built-up edge and surface scratching. Tool geometry and air or coolant direction should be selected with chip travel in mind, especially in deep features. Flute Geometry and Edge Sharpness Choose Enough Chip Space for the Operation Copper and ductile brass grades may require generous flute space so chips can leave the cutting zone before they are recut. A low-flute-count tool can be useful when chip evacuation is the primary limitation, but the correct flute count also depends on rigidity, engagement, feed, finish, and feature geometry. For a deep pocket or slot, prioritize a toolpath and geometry that provide a clear chip path. For a light finishing pass, a different flute configuration may be preferred if it provides the required surface quality without creating excess rubbing. Favor a Clean, Sharp Cutting Edge A sharp edge generally helps shear copper and brass rather than push or smear them. Excessive edge rounding can increase rubbing and heat. However, sharpness must be balanced against the risk of edge damage in interrupted cuts, cast surfaces, abrasive inclusions, or unstable fixtures. The best edge preparation is application-dependent. A stable finishing cut may benefit from a very sharp edge, while a roughing operation with impact risk may require controlled edge reinforcement. Request the intended edge preparation when comparing tools rather than judging only by the product title. Consider Polished Flutes and Rake Surfaces A smooth flute and rake surface can reduce friction and help chips slide away from the cutting edge. This is particularly relevant when the material tends to adhere or when the tool is used in a narrow cavity with limited chip clearance. Polishing alone does not replace the need for suitable flute volume, coolant, or air blast, but it can support cleaner chip transport. Coating and Substrate Considerations Copper alloy applications do not always benefit from the same coating choices used for hardened steel. The dominant issue may be adhesion and friction rather than oxidation or high-temperature wear. In some applications, uncoated polished carbide is appropriate because the sharp, low-friction surface is more important than a hard coating layer. For abrasive copper alloys, bronze grades, or materials containing hard particles, a coating or substrate selected for wear resistance may be useful. The correct choice depends on the exact alloy and failure mode. Do not assume that a coating marketed for hardened steel will automatically improve copper machining, and do not assume that an uncoated tool is correct for every bronze or filled alloy. When comparing copper tools with End Mills for Aluminum, use the aluminum tool as a reference only, not as an automatic substitute. Both material groups can be adhesion-prone, but the exact chip form, edge condition, and surface requirement may differ. Parameter Strategy for Copper and Brass Milling Start With the Actual Tool and Alloy Cutting data should be treated as a starting reference, not a guaranteed setting. The appropriate speed, feed, radial engagement, and axial depth depend on tool diameter, flute count, stickout, machine rigidity, workholding, alloy grade, and coolant or air-blast conditions. Validate the starting range on the actual machine before making it a standard process. Avoid Rubbing and Dwell If the tool spends too much time sliding along the surface, adhesion and smearing become more likely. Check whether the toolpath includes dwell at corners, excessive radial engagement, or a feed value that is too low for the selected edge geometry. A modest, controlled chip load is usually preferable to a cut dominated by rubbing, but the exact value must be validated for the tool and material. Control Chip Evacuation Direct air or coolant so chips move away from the cutting zone rather than being pushed back into the pocket. If chips are long, review flute volume, toolpath engagement, and the conditions that determine chip formation. Increasing fluid pressure without correcting nozzle direction or chip path may produce little improvement. Change One Variable at a Time When troubleshooting built-up edge, burrs, or poor finish, change only one major variable at a time: tool geometry, coating, speed, feed, engagement, or chip evacuation. Document the result. This makes it possible to identify the actual improvement instead of attributing every change to the last tool purchased. Toolholding, Workholding, and Feature Stability Even a well-selected tool can fail when the setup is unstable. Check tool runout, holder cleanliness, clamping length, and the shortest practical tool projection. Thin copper components and unsupported walls can deflect under cutting pressure, leaving burrs or dimensional error that look like a tool problem. For holes and finishing operations, coordinate the milling process with Carbide Drills and Carbide Reamers. A poor pre-hole or unstable entry can reduce the performance of the finishing tool even when the reamer itself is suitable. A Practical Selection and Troubleshooting Sequence Confirm the exact copper, brass, bronze, or copper-alloy grade and condition. Identify the dominant failure: adhesion, burrs, poor finish, chip packing, chipping, or dimensional drift. Select flute count and chip space based on engagement and chip travel, not on flute count alone. Review edge sharpness, rake surface, flute polish, coating, and substrate together. Check runout, overhang, workholding, and thin-wall support. Establish a conservative starting process and validate it on the actual setup. Adjust one variable at a time and record chip form, finish, burr condition, load behavior, and tool wear. Common Mistakes to Avoid Treating All Copper Alloys as Pure Copper Brass, bronze, and specialized copper alloys can produce very different chips and wear mechanisms. A recommendation for one grade should not be transferred automatically to another. Choosing Coating Before Identifying the Failure Mode If adhesion is the primary issue, friction and edge sharpness may deserve attention before thermal coating performance. If abrasion is dominant, the solution may require a different substrate or wear-resistant coating. Diagnose first. Using a Dull Tool for a Finishing Operation A worn edge can rub, smear, and create burrs even when the tool still appears usable. Replace or recondition the tool based on the required surface and dimensional result, not only on visible fracture. Ignoring Chip Travel in Pockets and Slots Long chips that remain in the cavity will be recut. Review toolpath direction, flute space, air blast, coolant placement, and the ability of the machine to clear chips. Copying Parameters From Steel or Aluminum Without Validation Copper alloy behavior is not identical to steel or aluminum. Use supplier data as a starting reference and confirm the process on the actual machine, workholding, and material grade. FAQ What type of carbide end mill is commonly used for copper? A sharp, low-friction tool with suitable chip space is often considered for copper, but the correct flute count, edge preparation, coating, and substrate depend on the exact alloy and operation. Confirm the choice against the material grade and feature geometry. Why does copper create built-up edge on the tool? Built-up edge is commonly associated with adhesion, rubbing, heat concentration, poor chip evacuation, or an edge condition that is not suited to the material. Review sharpness, flute polish, toolpath engagement, and validated parameters before changing coating alone. Is an uncoated carbide end mill suitable for brass and copper alloys? It can be suitable in some applications where a sharp, polished, low-friction edge is the priority. Abrasive bronze or filled copper alloys may require a different wear strategy. The exact recommendation should be confirmed for the specific grade and failure mode. How can I reduce burrs when milling copper? Check tool sharpness, runout, exit engagement, workpiece support, radial engagement, and feed direction. A finishing pass may help, but burr reduction is usually more reliable when the edge and toolpath are stable from the beginning. What information should I provide when requesting a copper alloy tool recommendation? Provide the exact alloy and condition, tool diameter and flute count, feature geometry, tool overhang, machine and holder details, current parameters, coolant or air-blast method, chip form, and photographs of the finish or worn edge. Conclusion Choosing carbide end mills for copper and brass machining requires more than selecting a standard tool for a soft material. The best starting point is to identify the alloy, failure mode, chip behavior, and setup stability. Sharp and suitable geometry, sufficient chip space, controlled friction, reliable evacuation, and validated parameters work together to reduce built-up edge, burrs, smearing, chipping, and inconsistent tool life. If your copper or brass operation has adhesion, burr, chip evacuation, surface-finish, or tool-life problems, Contact Supal with the material grade, feature geometry, current tool, parameters, and failure photos. This information helps evaluate a practical tool and process starting point for on-machine validation.
2026

10/01

탄화화물 재미어 왈가왈부 와 과대 구멍: 문제 해결 지침
카바이드 리머 챗터 및 과대 치수 구멍: 문제 해결 가이드 리밍은 종종 간단한 마무리 작업으로 취급됩니다. 구멍을 뚫고 리머를 돌리면 치수와 표면 마감이 개선될 것으로 기대합니다. 실제로는 카바이드 리밍은 여유량, 정렬, 강성, 냉각수 공급, 날 형상 및 매개변수 안정성에 민감합니다. 이러한 변수 중 하나라도 잘못되면 공정에서 챗터 자국, 과대 치수 구멍, 불량한 원형도, 테이퍼 구멍, 날 칩핑 또는 예상보다 짧은 공구 수명이 발생할 수 있습니다. CNC 기계공, 공정 엔지니어 및 구매 엔지니어에게 핵심은 다음과 같습니다. 리머는 모든 드릴링 문제를 해결하지 못합니다. 리머는 준비된 구멍을 개선할 수 있지만 심하게 정렬되지 않거나 긁히거나 치수가 작거나 벨 마우스 모양이거나 불안정한 사전 구멍을 안정적으로 수정할 수는 없습니다. 이 가이드에서는 카바이드 리머 챗터 및 구멍 공차 문제를 단계별로 진단하는 방법을 설명하므로 수정 조치는 추측이 아닌 실패 모드를 기반으로 합니다. 리밍 문제가 진단하기 어려운 이유 카바이드 리머는 여러 개의 날이 동시에 절삭하고 소량의 재료만 제거합니다. 이 작업은 드릴링이나 밀링에 비해 가볍기 때문에 많은 작업장에서 리밍은 관대해야 한다고 가정합니다. 실제로 소량의 재료 여유량과 엄격한 공차 목표는 공정을 덜 관대하게 만듭니다. 리밍 여유량이 너무 작으면 공구가 절삭 대신 마찰될 수 있습니다. 여유량이 너무 크면 절삭 날이 과부하될 수 있습니다. 드릴링된 구멍이 직선이 아니면 리머가 기존의 오차를 따르거나 불균일하게 절삭해야 할 수 있습니다. 홀더나 고정 장치에 강성이 부족하면 작은 진동이 구멍 내부의 눈에 보이는 챗터 선으로 나타날 수 있습니다. 이것이 동일한 리머가 한 설정에서는 우수한 마감을 생성하고 동일한 공칭 구멍 직경의 다른 설정에서는 실패하는 이유입니다. 카바이드 리밍의 일반적인 증상 구멍 내부의 챗터 자국 챗터 자국은 일반적으로 구멍 벽에 반복적인 나선형 또는 다각형 모양의 패턴으로 나타납니다. 이는 절삭 중에 공구, 홀더, 공작물 또는 기계 구조가 진동하고 있음을 나타냅니다. 챗터는 과도한 여유량, 불충분한 강성, 불량한 정렬, 잘못된 속도 또는 불안정한 사전 구멍으로 인해 발생할 수 있습니다. 리밍 후 과대 치수 구멍 과대 치수 구멍은 공구 런아웃, 정렬 불량, 과도한 절삭 압력, 열팽창 또는 리머와 구멍 벽 사이에 갇힌 칩으로 인해 발생할 수 있습니다. 과대 치수 구멍이 일관되게 반복되면 리머 직경이 잘못되었다고 가정하기 전에 런아웃을 측정하고 사전 구멍 상태를 확인하십시오. 불량한 표면 마감 리밍 후 불량한 표면 마감은 빌드업 에지, 부적절한 냉각수, 칩 재절삭, 불량한 드릴 준비 또는 마모된 절삭 날에서 발생할 수 있습니다. 리머가 불균일한 재료를 제거하도록 강제되면 공구가 날카롭더라도 표면 마감이 종종 악화됩니다. 짧거나 일관되지 않은 공구 수명 동일한 응용 분야에서 한 리머가 다른 리머보다 훨씬 오래 지속된다면 기계 설정, 구멍 준비, 냉각수 공급 및 부품 재료 변동을 검토하십시오. 공구 코팅 및 카바이드 등급이 중요하지만 공정 불안정성이 종종 먼저 제거해야 할 사항입니다. 날 칩핑 카바이드 리머의 날 칩핑은 종종 충격, 간헐적 절삭, 과도한 여유량, 불량한 진입 또는 공작물의 단단한 포함물로 인해 발생합니다. 리머는 마무리 공구이며, 큰 드릴링 오류를 수정하거나 많은 양의 재료를 제거하도록 설계되지 않았습니다. 근본 원인 1: 잘못된 리밍 여유량 사전 구멍 여유량은 리밍에서 가장 중요한 변수 중 하나입니다. 재료가 너무 적으면 마찰, 열 및 불량한 마감이 발생할 수 있습니다. 재료가 너무 많으면 절삭 날이 과부하되어 챗터 또는 칩핑이 발생할 수 있습니다. 모든 직경, 재료 및 리머 설계에 맞는 보편적인 여유량은 없습니다. 시작 원칙으로, 소형 구멍은 일반적으로 더 작은 여유량이 필요하며, 대형 구멍은 더 많은 재료 제거를 허용할 수 있습니다. 그러나 올바른 값은 공작물 재료, 구멍 깊이, 공구 형상, 냉각수 방법 및 공차 목표에 따라 달라집니다. 다른 작업의 값을 복사하는 대신 항상 실제 기계 및 고정 장치에서 여유량을 검증하십시오. 문제 해결 시 리밍 전 실제 드릴링된 구멍 직경과 최종 목표를 비교하십시오. 부품마다 사전 구멍 크기가 다르면 리밍 결과도 달라집니다. 근본 원인 2: 불량한 사전 구멍 품질 리머는 안정적인 안내가 필요합니다. 드릴링된 구멍이 이미 위치에서 벗어나거나, 테이퍼지거나, 긁히거나, 심하게 가공 경화된 경우 리밍이 훨씬 더 어려워집니다. 리머를 비난하기 전에 드릴링 공정을 검사하십시오. 드릴이 둥글고 직선인 구멍을 생성하는지, 칩이 벽을 긁고 있는지, 드릴이 진입 시 흔들리는지 확인하십시오. 구멍 생성 공정 제어를 위해, 카바이드 드릴 및 리머는 관련 없는 공구가 아닌 시스템으로 선택해야 합니다. 드릴이 심한 칩 긁힘이나 일관되지 않은 구멍 크기를 남기면 리머가 결함을 수리할 만큼 제어력이 없을 수 있습니다. 먼저 드릴링 안정성을 개선한 다음 리밍 패스를 평가하십시오. 근본 원인 3: 런아웃 및 정렬 불량 런아웃은 과대 치수 구멍과 불균일한 공구 마모를 생성하는 가장 빠른 방법 중 하나입니다. 홀더 또는 스핀들의 약간의 런아웃은 다른 절삭 날보다 더 많은 작업을 수행하게 만들 수 있습니다. 이는 불균일한 절삭 압력, 불량한 원형도 및 짧은 공구 수명을 유발합니다. 가능한 경우 공구 생크 및 절삭부 근처에서 런아웃을 확인하십시오. 홀더 상태, 콜릿 청결도, 스핀들 상태 및 공구가 충분한 접촉 길이로 고정되었는지도 검토하십시오. 정밀 구멍의 경우 공구 홀딩 시스템은 리머 자체만큼 중요합니다. 리머가 스핀들 경로와 동축이 아닌 구멍에 들어갈 때 정렬 불량이 발생할 수도 있습니다. 이는 이전 작업, 고정 장치 또는 긴 도달 거리 설정이 편향을 유발할 때 일반적입니다. 근본 원인 4: 속도, 이송 및 절삭 안정성 리밍 매개변수는 마찰이나 진동 없이 깨끗하게 절삭할 수 있을 만큼 안정적이어야 합니다. 너무 높은 속도는 열을 증가시키고 일부 재료에서 챗터를 악화시킬 수 있습니다. 너무 낮은 이송은 절삭 대신 마찰을 유발할 수 있습니다. 너무 높은 이송은 날을 과부하하고 표면 마감을 손상시킬 수 있습니다. 문제 해결을 위해 한 번에 하나의 변수만 조정하십시오. 챗터가 나타나면 속도를 약간 줄이는 것이 도움이 될 수 있지만, 강성과 여유량이 이미 합리적인 경우에만 해당됩니다. 공구가 마찰되고 열을 발생시키면 안전 범위 내에서 이송을 늘리는 것이 때때로 절삭 작용을 개선할 수 있습니다. 매개변수 변경은 실제 부품 재료에서 시험 절삭을 통해 검증해야 합니다. 일반적인 속도 및 이송 표를 최종 값으로 사용하지 마십시오. 이를 시작 참조로 취급하고 구멍 크기, 깊이, 기계 강성, 냉각수 및 공차 요구 사항에 따라 조정하십시오. 근본 원인 5: 냉각수 및 칩 제어 리밍은 드릴링보다 재료를 덜 제거하지만 칩은 여전히 중요합니다. 구멍 내부에 갇힌 미세 칩이나 입자는 벽을 긁고 절삭 날을 손상시킬 수 있습니다. 냉각수는 칩을 배출하고, 열을 줄이며, 절삭 영역을 안정화하는 데 도움이 됩니다. 블라인드 구멍의 경우 칩이 구멍 바닥에서 빠져나갈 공간이 제한되어 칩 배출이 더 어려워집니다. 냉각수 방향, 압력 및 흐름을 신중하게 검토해야 합니다. 드릴링에서 구멍에 칩이 남아 있으면 리밍 전에 구멍을 청소하거나 헹구십시오. 냉각수 농도 및 여탕도 중요합니다. 오염된 냉각수는 연마성 입자를 구멍으로 다시 운반하여 표면 마감 및 공구 수명에 영향을 줄 수 있습니다. 근본 원인 6: 리머 형상 및 응용 분야 적합성 다양한 카바이드 리머는 다양한 응용 분야에 맞게 설계되었습니다. 플루트 설계, 리드 각도, 마진 설계, 날 준비 및 코팅과 같은 요소는 절삭 안정성 및 칩 배출에 영향을 줄 수 있습니다. 스루 홀용 리머는 블라인드 홀에서 동일하게 작동하지 않을 수 있습니다. 알루미늄에 최적화된 리머는 스테인리스강 또는 경화된 재료에 이상적이지 않을 수 있습니다. 긴 리머는 강성 및 런아웃에 대한 추가 주의가 필요할 수 있습니다. 공급업체와 리머 문제에 대해 논의할 때 공작물 재료, 사전 구멍 직경, 목표 공차, 구멍 깊이, 스루 홀 또는 블라인드 홀 조건, 냉각수 방법, 현재 매개변수 및 가능한 경우 구멍 표면 사진을 제공하십시오. 이 정보는 솔루션이 형상 변경, 매개변수 변경 또는 공정 수정인지 결정하는 데 도움이 됩니다. 실용적인 문제 해결 워크플로우 1단계: 사전 구멍 측정 마감된 구멍을 확인하기 전에 리밍 전에 드릴링되거나 보링된 구멍을 측정하십시오. 가능한 경우 직경, 원형도, 직선도 및 표면 상태를 기록하십시오. 사전 구멍이 불안정하면 먼저 수정하십시오. 2단계: 공구 런아웃 확인 실제 홀더에서 런아웃을 측정하십시오. 생크, 콜릿 및 홀더를 청소하십시오. 손상된 홀더 또는 마모된 콜릿을 교체하십시오. 런아웃이 줄어들고 과대 치수 구멍이 개선되면 리머가 주요 원인이 아닙니다. 3단계: 여유량 검토 실제 사전 구멍 직경과 리머 크기를 비교하십시오. 부품마다 여유량이 다르면 드릴링 또는 보링 작업이 일관되지 않은 이유를 파악하십시오. 4단계: 칩 및 표면 마감 검사 구멍에 갇힌 칩, 긁힘 또는 마찰 자국을 찾으십시오. 칩 긁힘이 나타나면 냉각수 배출 및 사전 구멍 청소를 개선하십시오. 5단계: 매개변수 점진적 조정 속도, 이송 또는 냉각수를 한 번에 하나씩 변경하십시오. 결과를 기록하십시오. 현재 설정이 명확하게 부적합하지 않는 한 공구 형상과 매개변수를 동시에 변경하지 마십시오. 6단계: 공구 선택 검토 공정이 안정적이지만 문제가 지속되면 리머 형상, 코팅, 플루트 스타일 및 날 준비를 검토하십시오. 관련 가공 및 마무리 응용 분야의 경우 Supal은 더 광범위한 CNC 공정 계획을 위해 카바이드 밀링 공구도 제공합니다. 피해야 할 일반적인 실수 실수 1: 리머가 불량한 구멍을 수정할 것으로 기대하는 것 리머는 마무리 공구이지 구조 공구가 아닙니다. 드릴링된 구멍이 심하게 중심에서 벗어나거나, 테이퍼지거나, 긁힌 경우 먼저 사전 구멍을 개선하십시오. 실수 2: 런아웃 무시 런아웃은 정확한 리머가 과대 치수로 절삭하게 만들 수 있습니다. 공구 자체에 문제가 있다고 가정하는 대신 항상 실제 홀더에서 공구를 측정하십시오. 실수 3: 여유량 너무 적게 사용 재료가 너무 적으면 마찰, 열 및 불량한 마감이 발생할 수 있습니다. 공구는 불규칙한 재료를 연마하는 것이 아니라 절삭해야 합니다. 실수 4: 여유량 너무 많이 사용 재료가 너무 많으면 절삭 날이 과부하되어 챗터, 칩핑 또는 불량한 원형도가 발생할 수 있습니다. 실수 5: 공정 확인 전에 리머 직경 변경 런아웃, 정렬 불량 또는 챗터로 인해 구멍이 과대 치수가 된 경우 공구 직경을 변경해도 근본적인 문제가 해결되지 않을 수 있습니다. 자주 묻는 질문 내 카바이드 리머가 과대 치수 구멍을 생성하는 이유는 무엇입니까? 일반적인 원인으로는 런아웃, 정렬 불량, 과도한 여유량, 불안정한 사전 구멍 품질, 갇힌 칩 또는 열 효과가 있습니다. 리머 직경이 잘못되었다고 가정하기 전에 런아웃과 사전 구멍 크기를 측정하십시오. 리머가 드릴 편차를 수정할 수 있습니까? 제한된 정도까지만 가능합니다. 드릴링된 구멍이 상당히 벗어나거나 직선이 아닌 경우 리머가 기존의 오차를 따를 수 있습니다. 먼저 드릴링 또는 보링 공정을 개선하십시오. 리밍 중 챗터의 원인은 무엇입니까? 챗터는 과도한 여유량, 불량한 강성, 잘못된 속도, 긴 공구 돌출, 불안정한 사전 구멍 형상 또는 스핀들과 구멍 사이의 불량한 정렬로 인해 발생할 수 있습니다. 리머 챗터를 멈추기 위해 속도를 줄여야 합니까, 아니면 이송을 줄여야 합니까? 때때로 속도를 줄이는 것이 도움이 되지만 항상 첫 번째 해결책은 아닙니다. 먼저 런아웃, 여유량, 홀더 강성 및 사전 구멍 품질을 확인하십시오. 너무 낮은 이송은 마찰을 유발할 수도 있습니다. 리머 문제 해결 지원을 요청할 때 어떤 정보를 보내야 합니까? 공작물 재료, 사전 구멍 직경, 목표 직경 및 공차, 구멍 깊이, 스루 홀 또는 블라인드 홀 조건, 냉각수 방법, 현재 속도/이송, 공구 돌출, 홀더 유형 및 구멍 표면 또는 마모된 리머 사진을 보내십시오. 결론 카바이드 리머 챗터, 과대 치수 구멍 및 짧은 공구 수명은 일반적으로 공구 문제뿐만 아니라 공정 문제입니다. 가장 효과적인 문제 해결 순서는 사전 구멍 측정, 런아웃 확인, 여유량 검토, 표면 마감 검사 및 매개변수를 한 번에 하나씩 조정하는 것입니다. 불안정한 구멍 공차, 챗터 자국 또는 짧은 리머 수명에 직면한 경우, Supal에 문의하여 공작물 재료, 사전 구멍 상태, 목표 공차, 현재 매개변수 및 실패 사진을 제공하십시오. Supal은 근본 원인이 여유량, 런아웃, 냉각수, 리머 형상 또는 전반적인 공정 안정성인지 평가하는 데 도움을 줄 수 있습니다.

2026

09/29